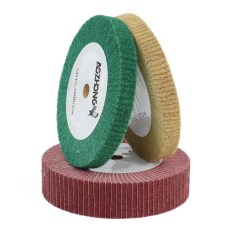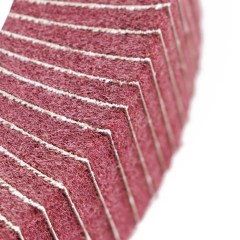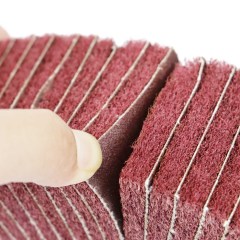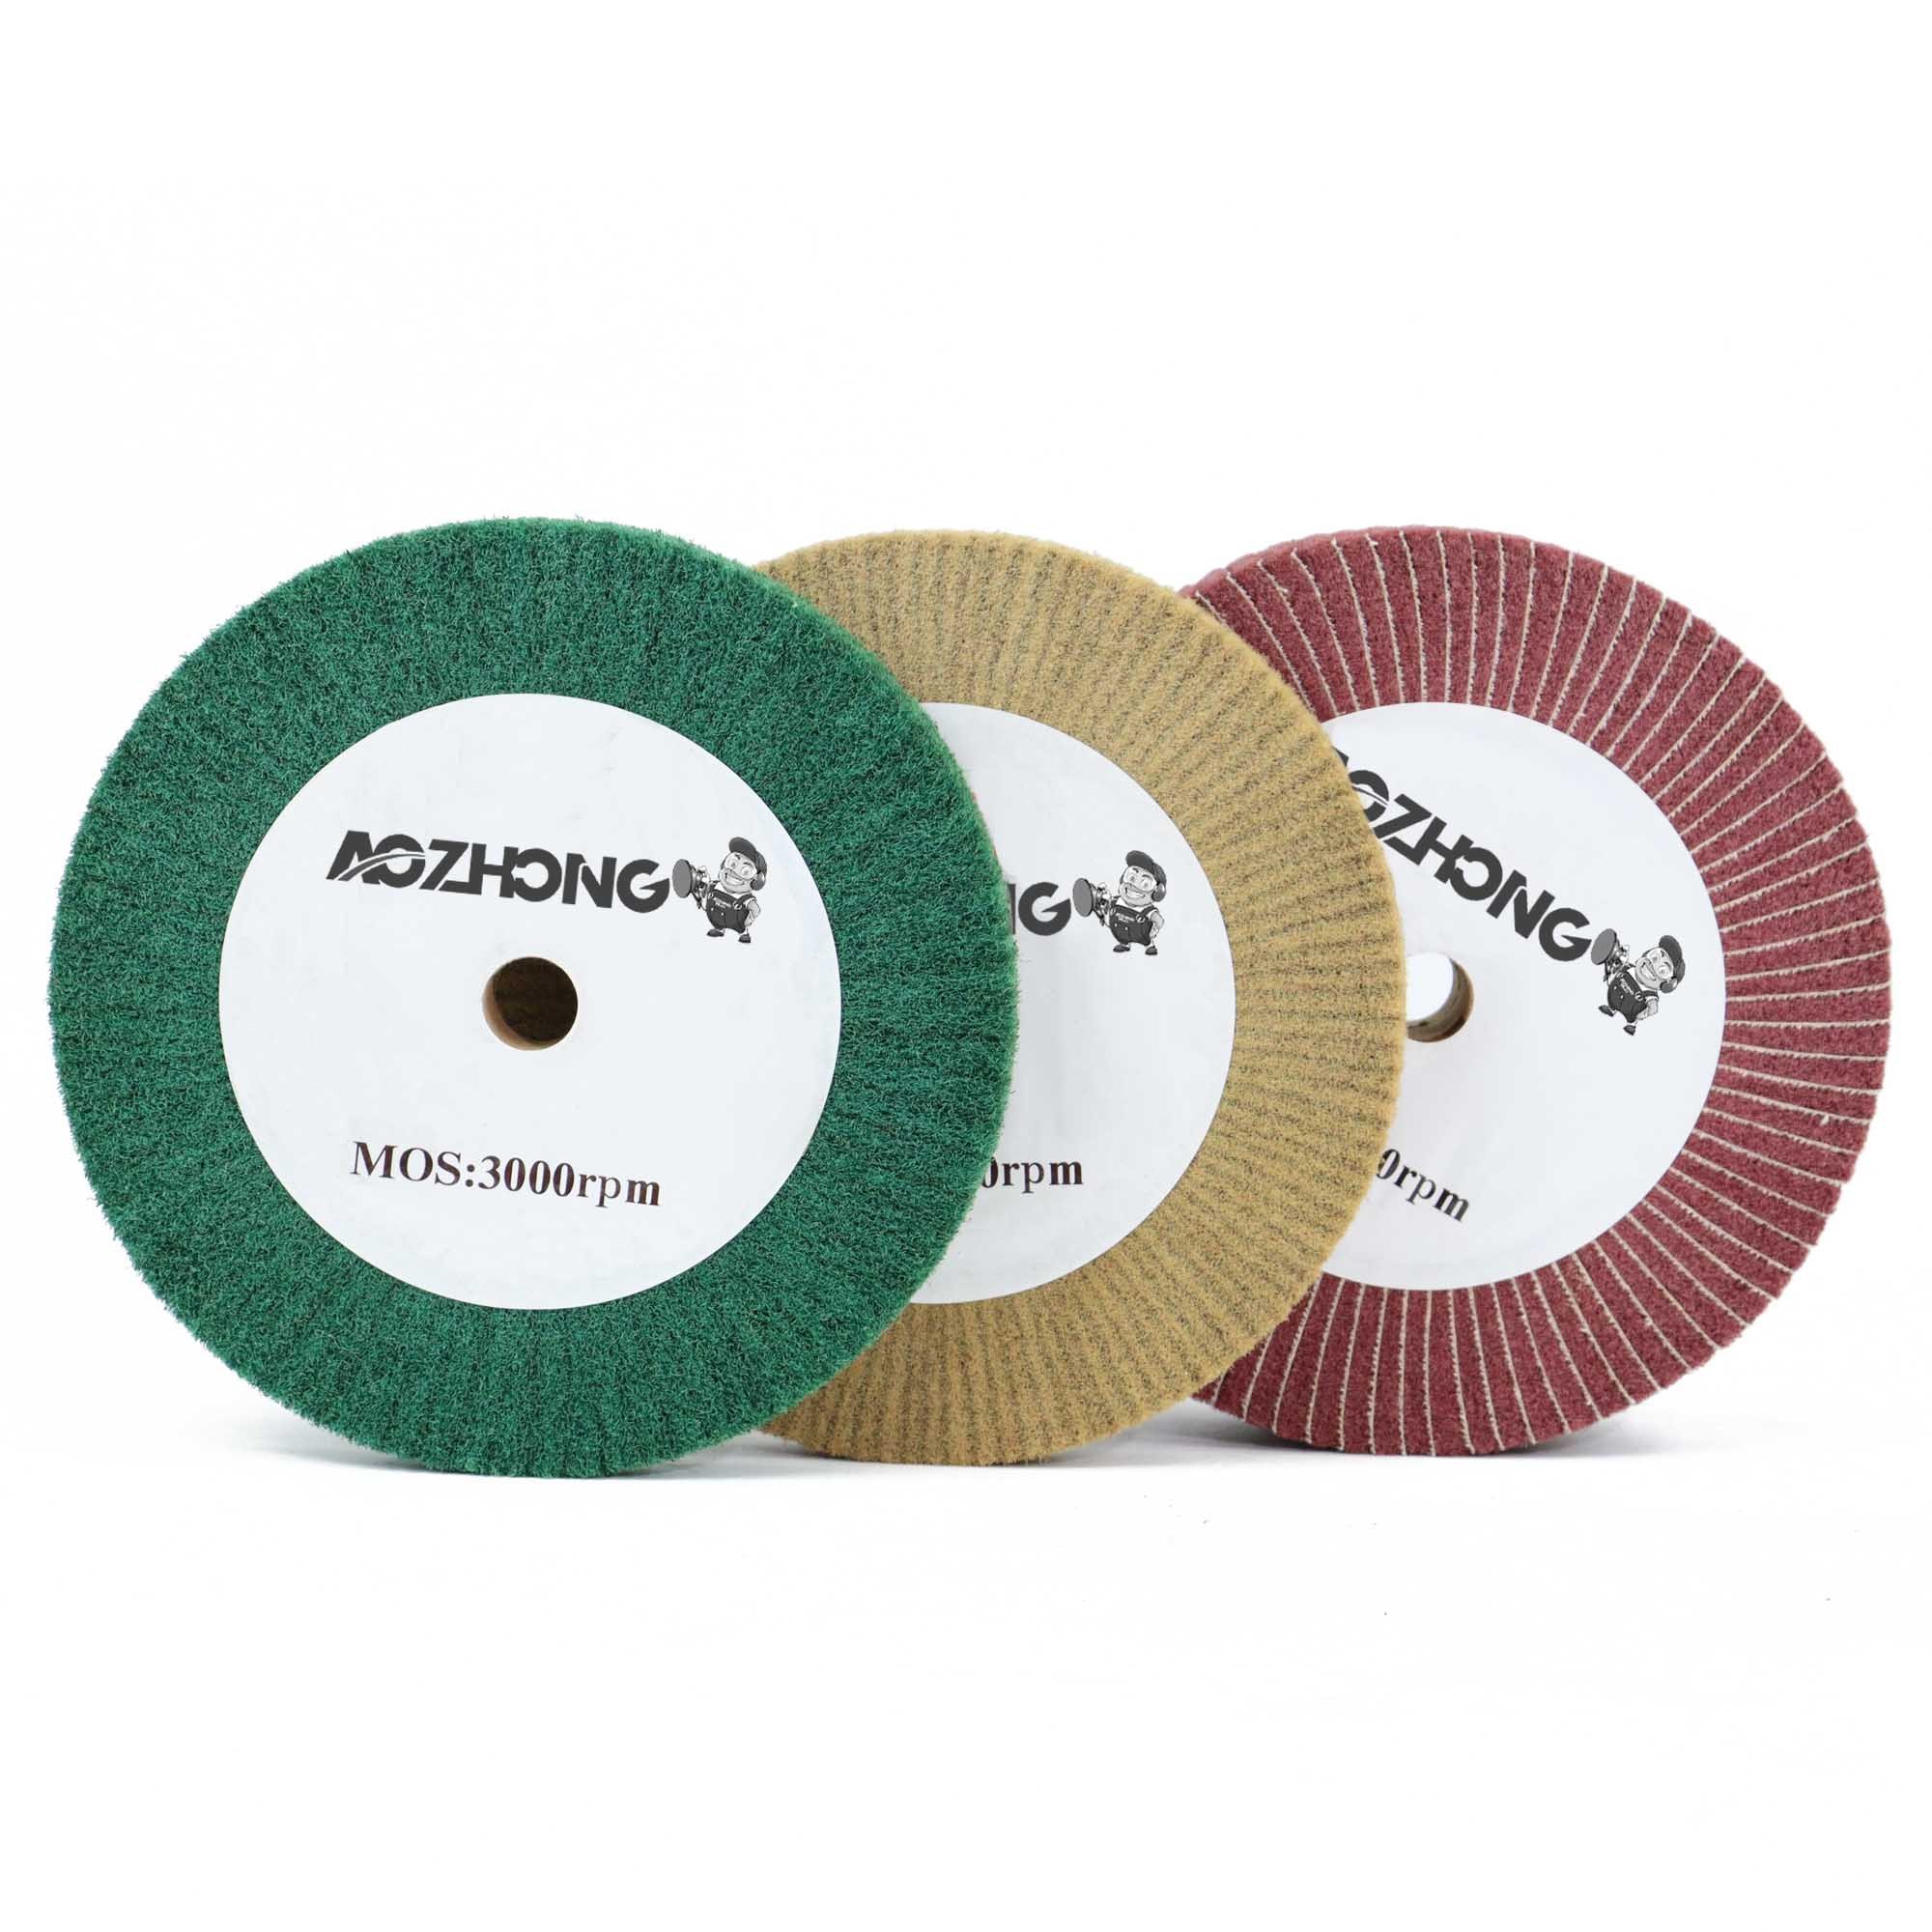
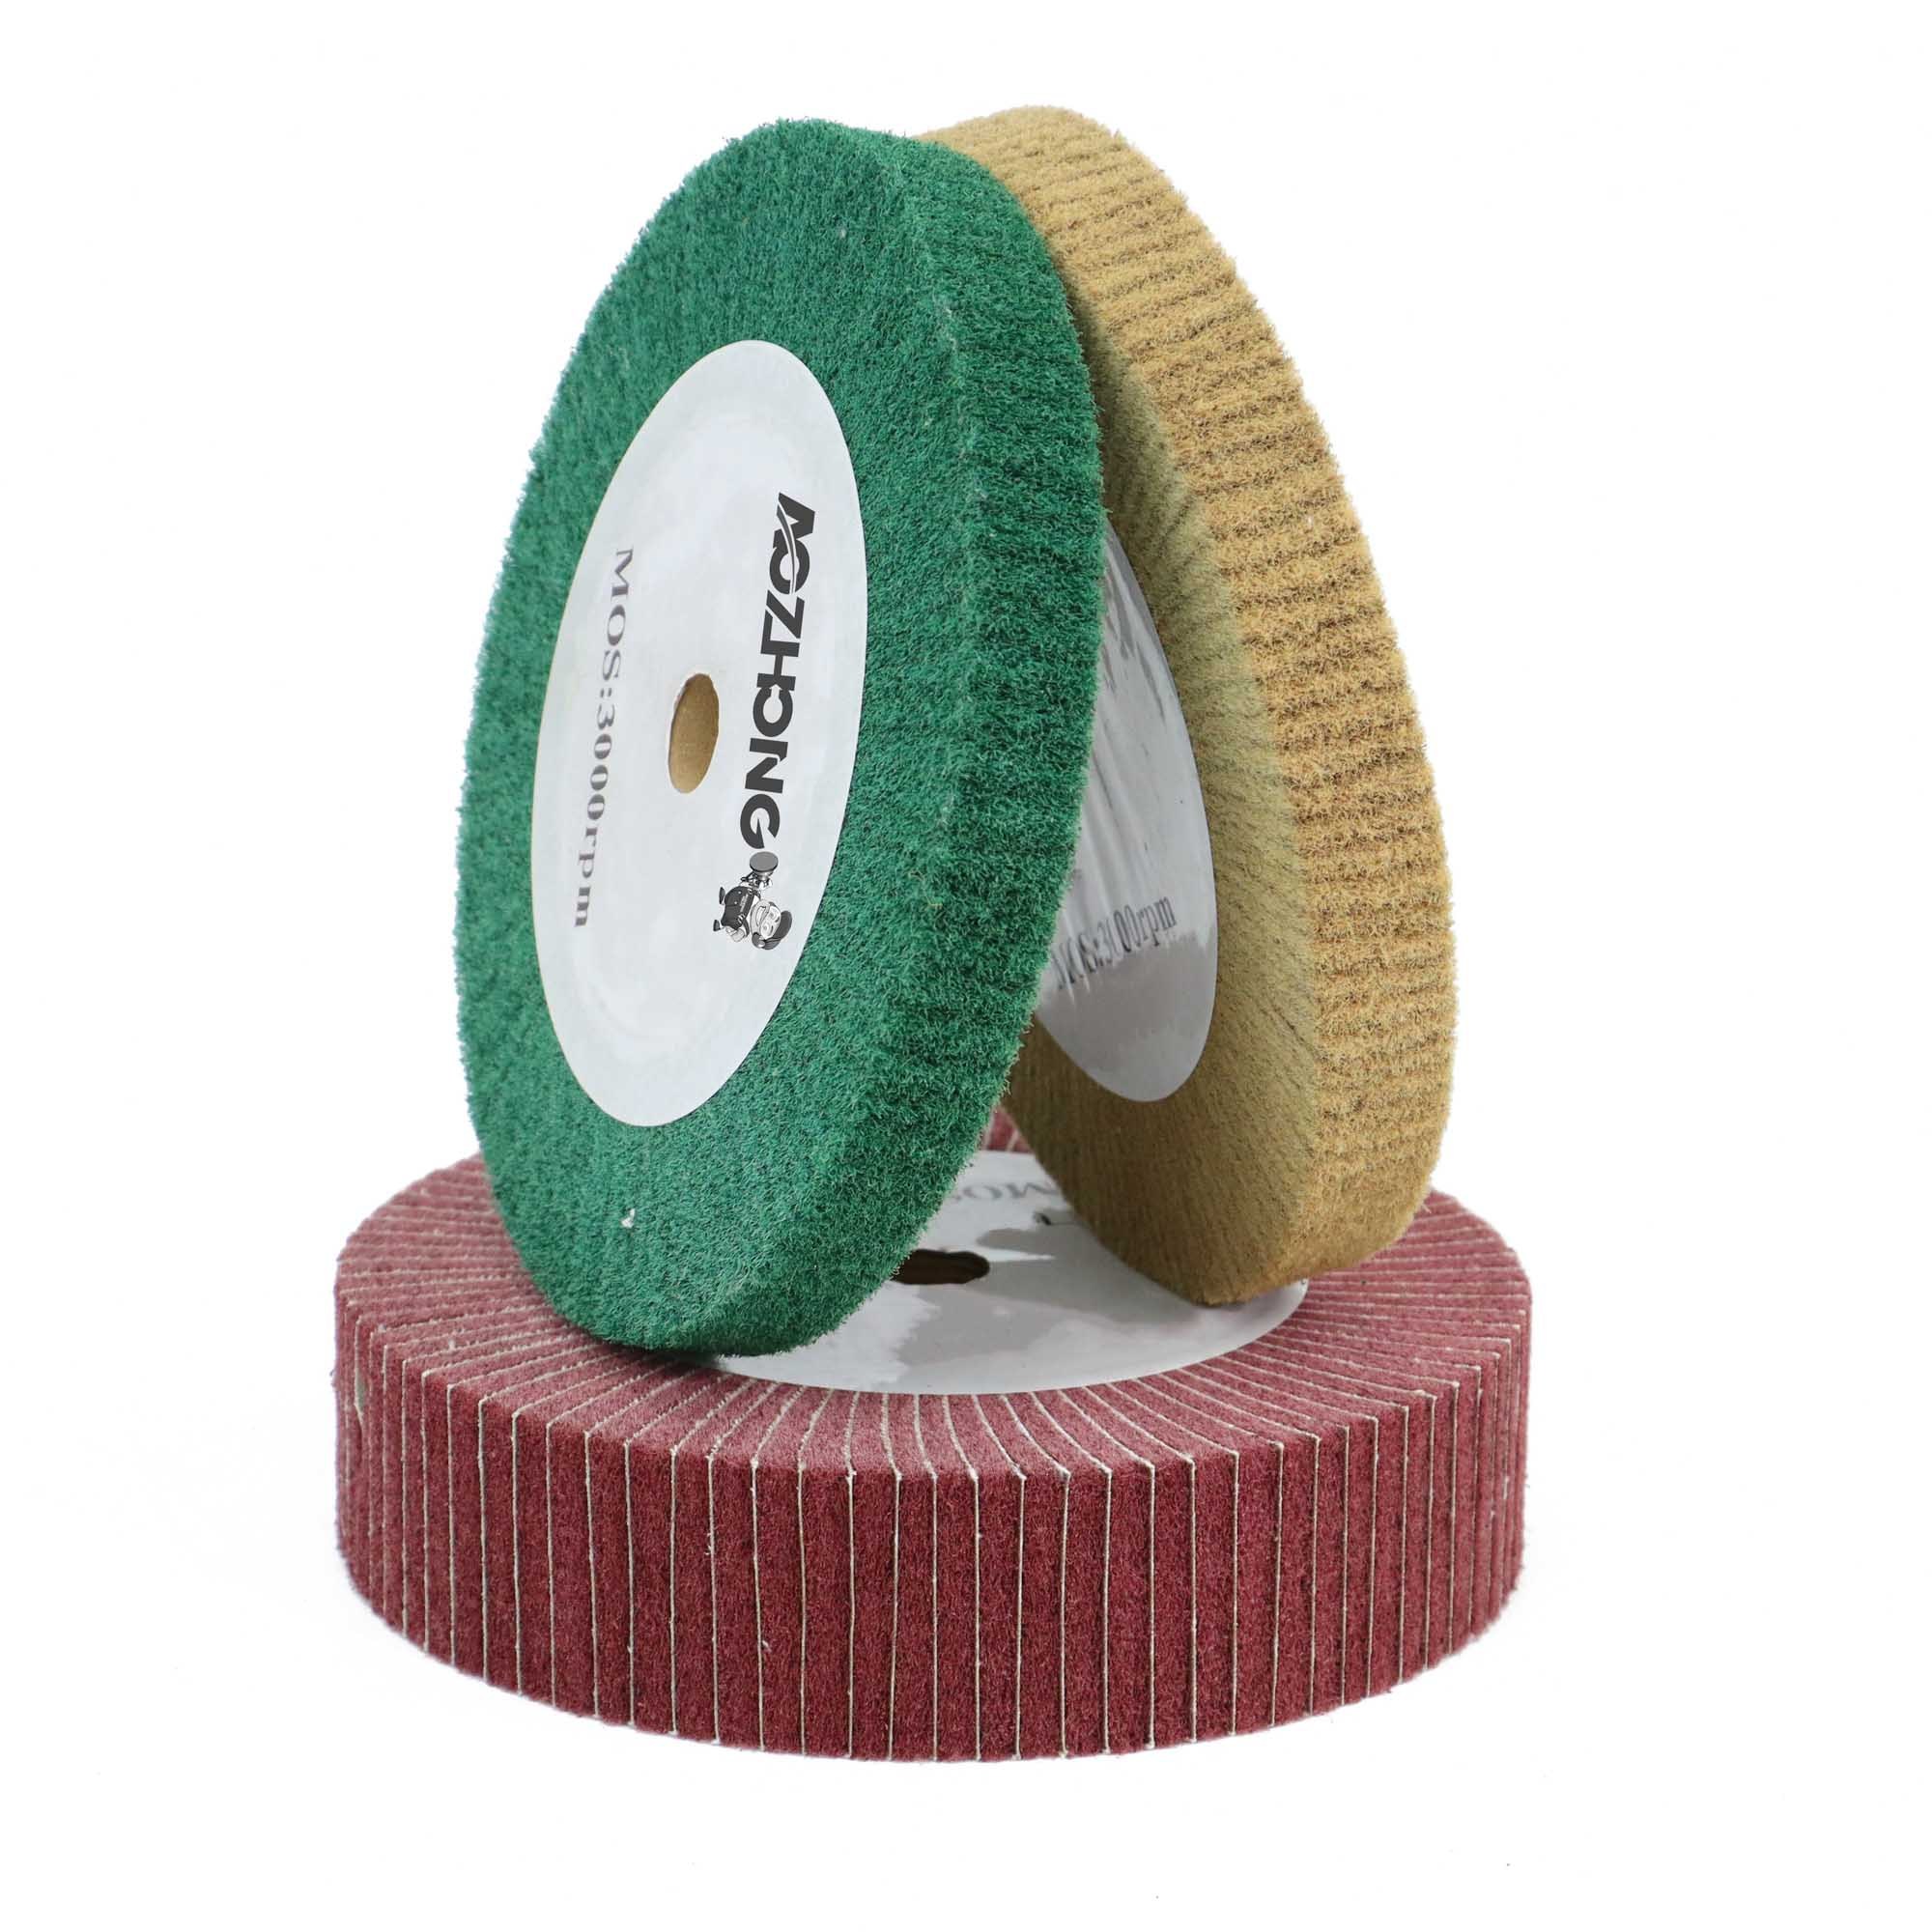
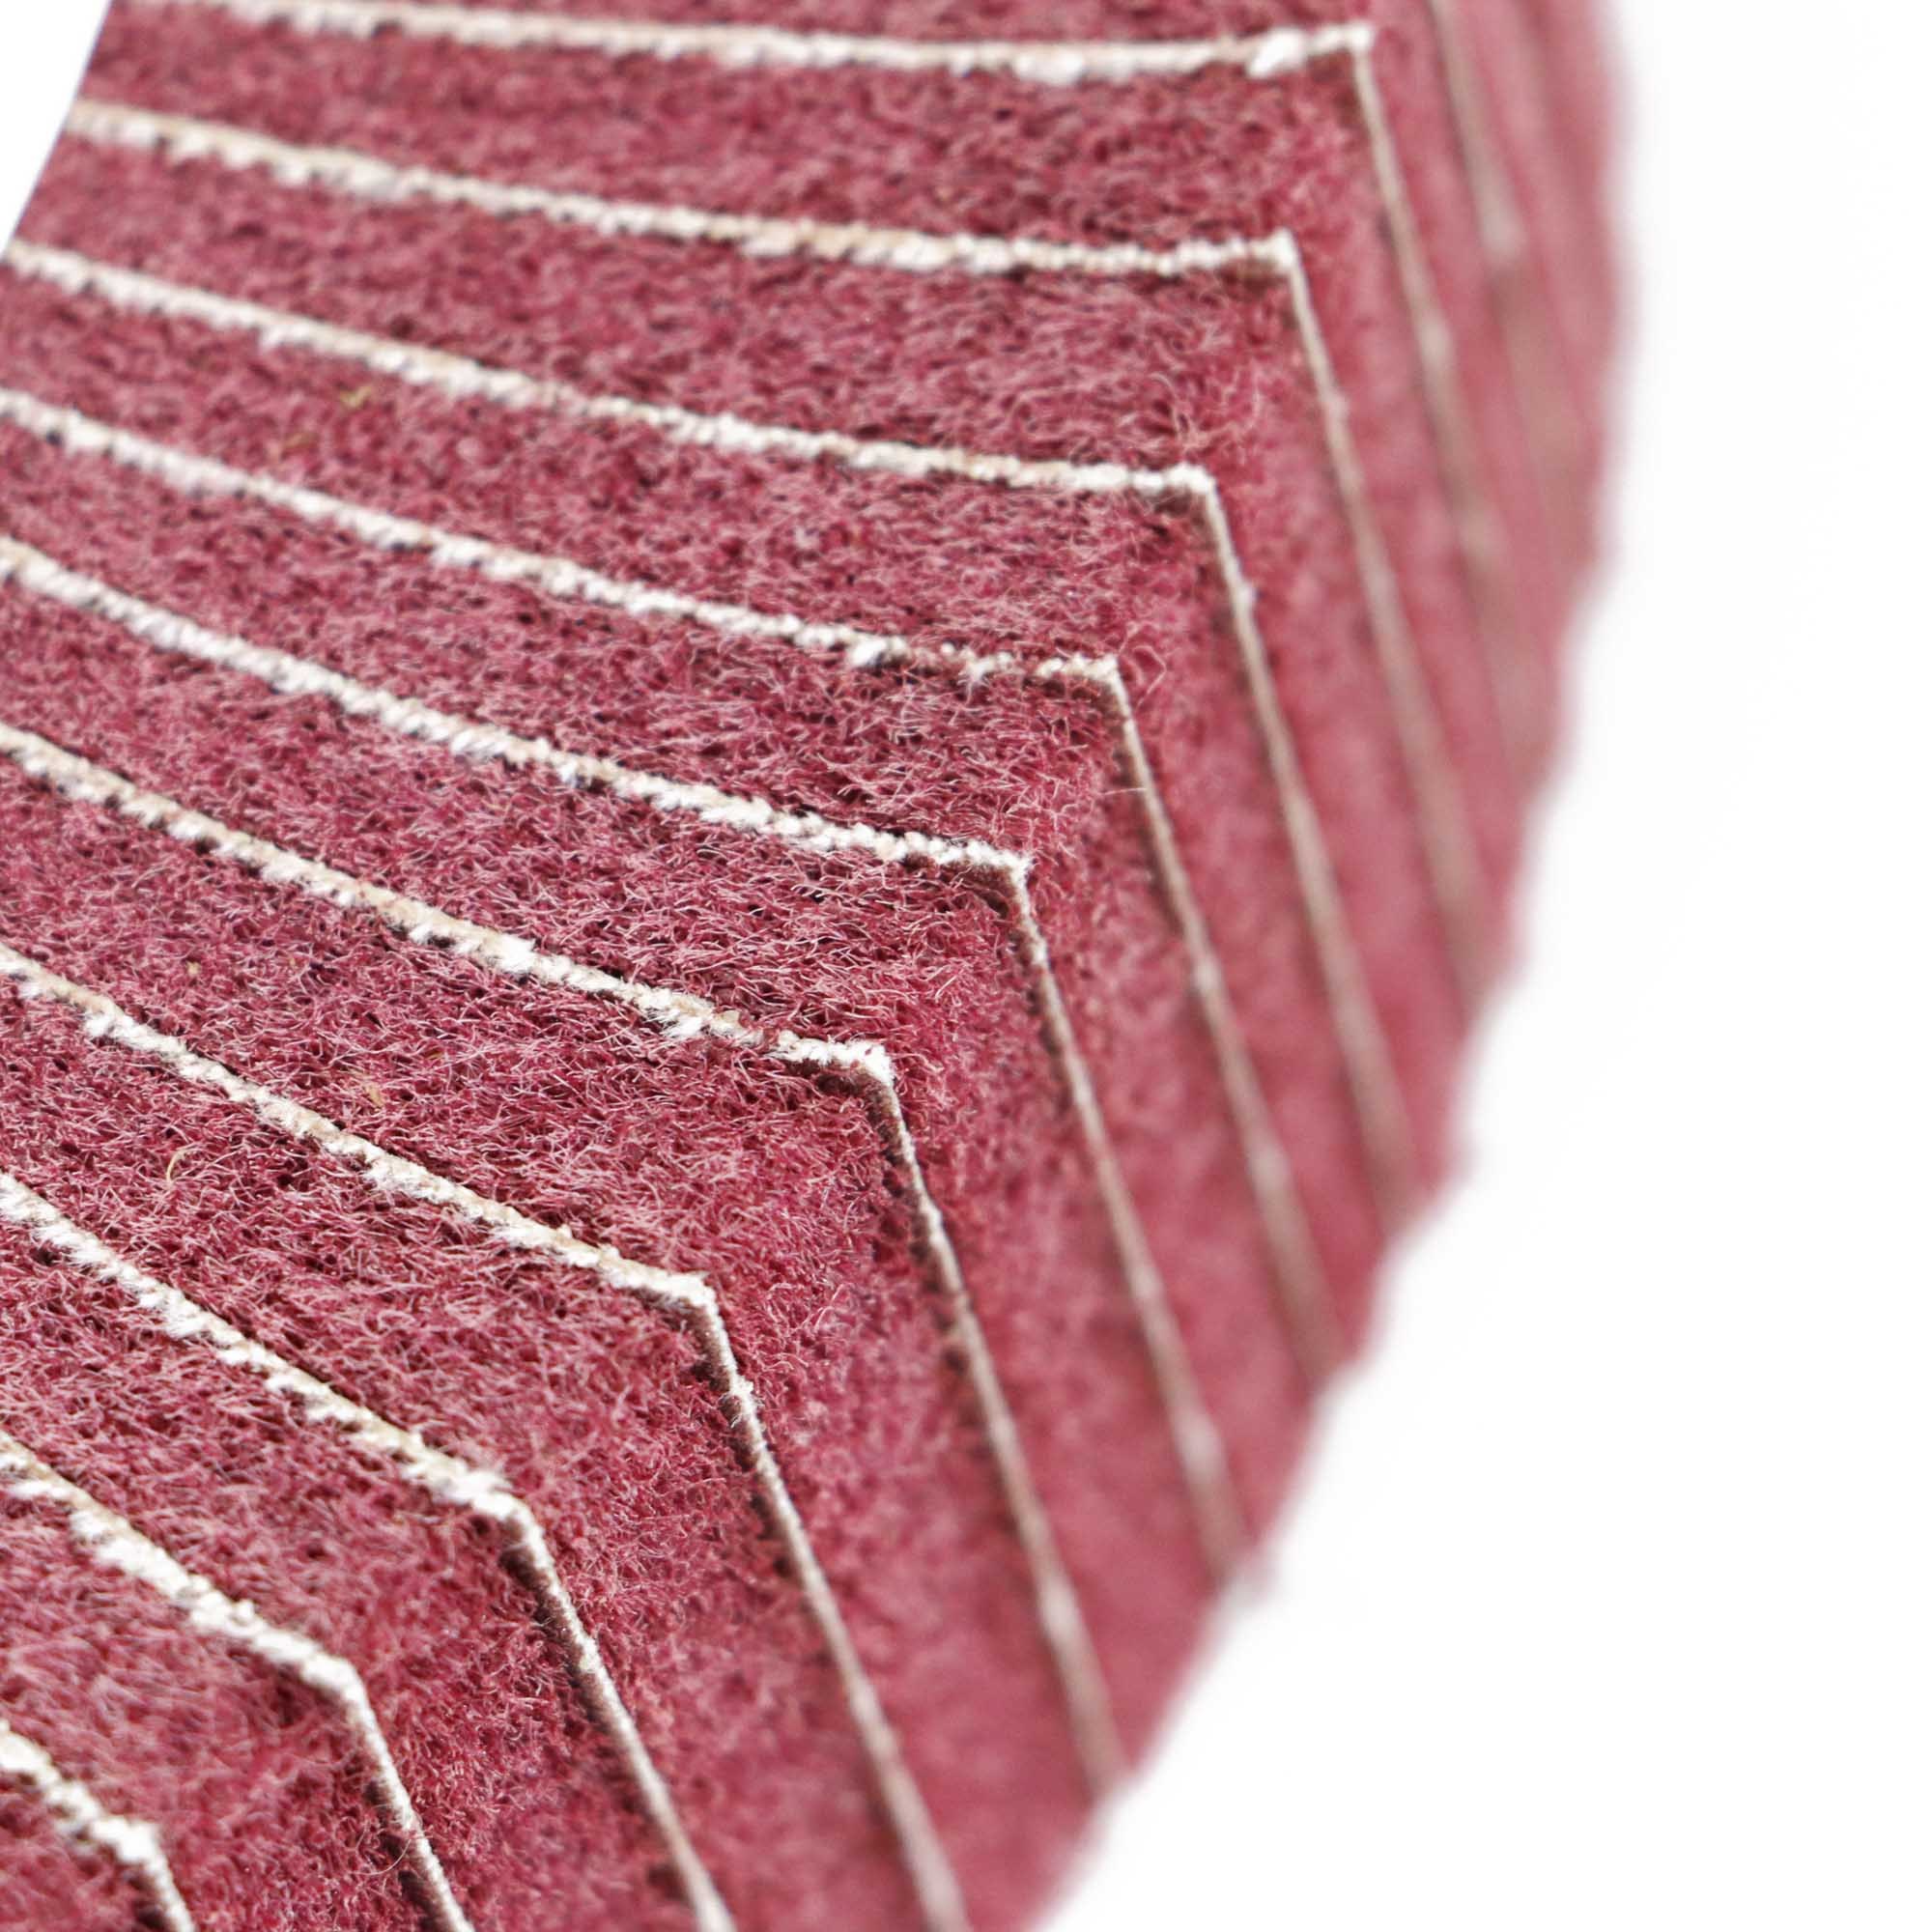
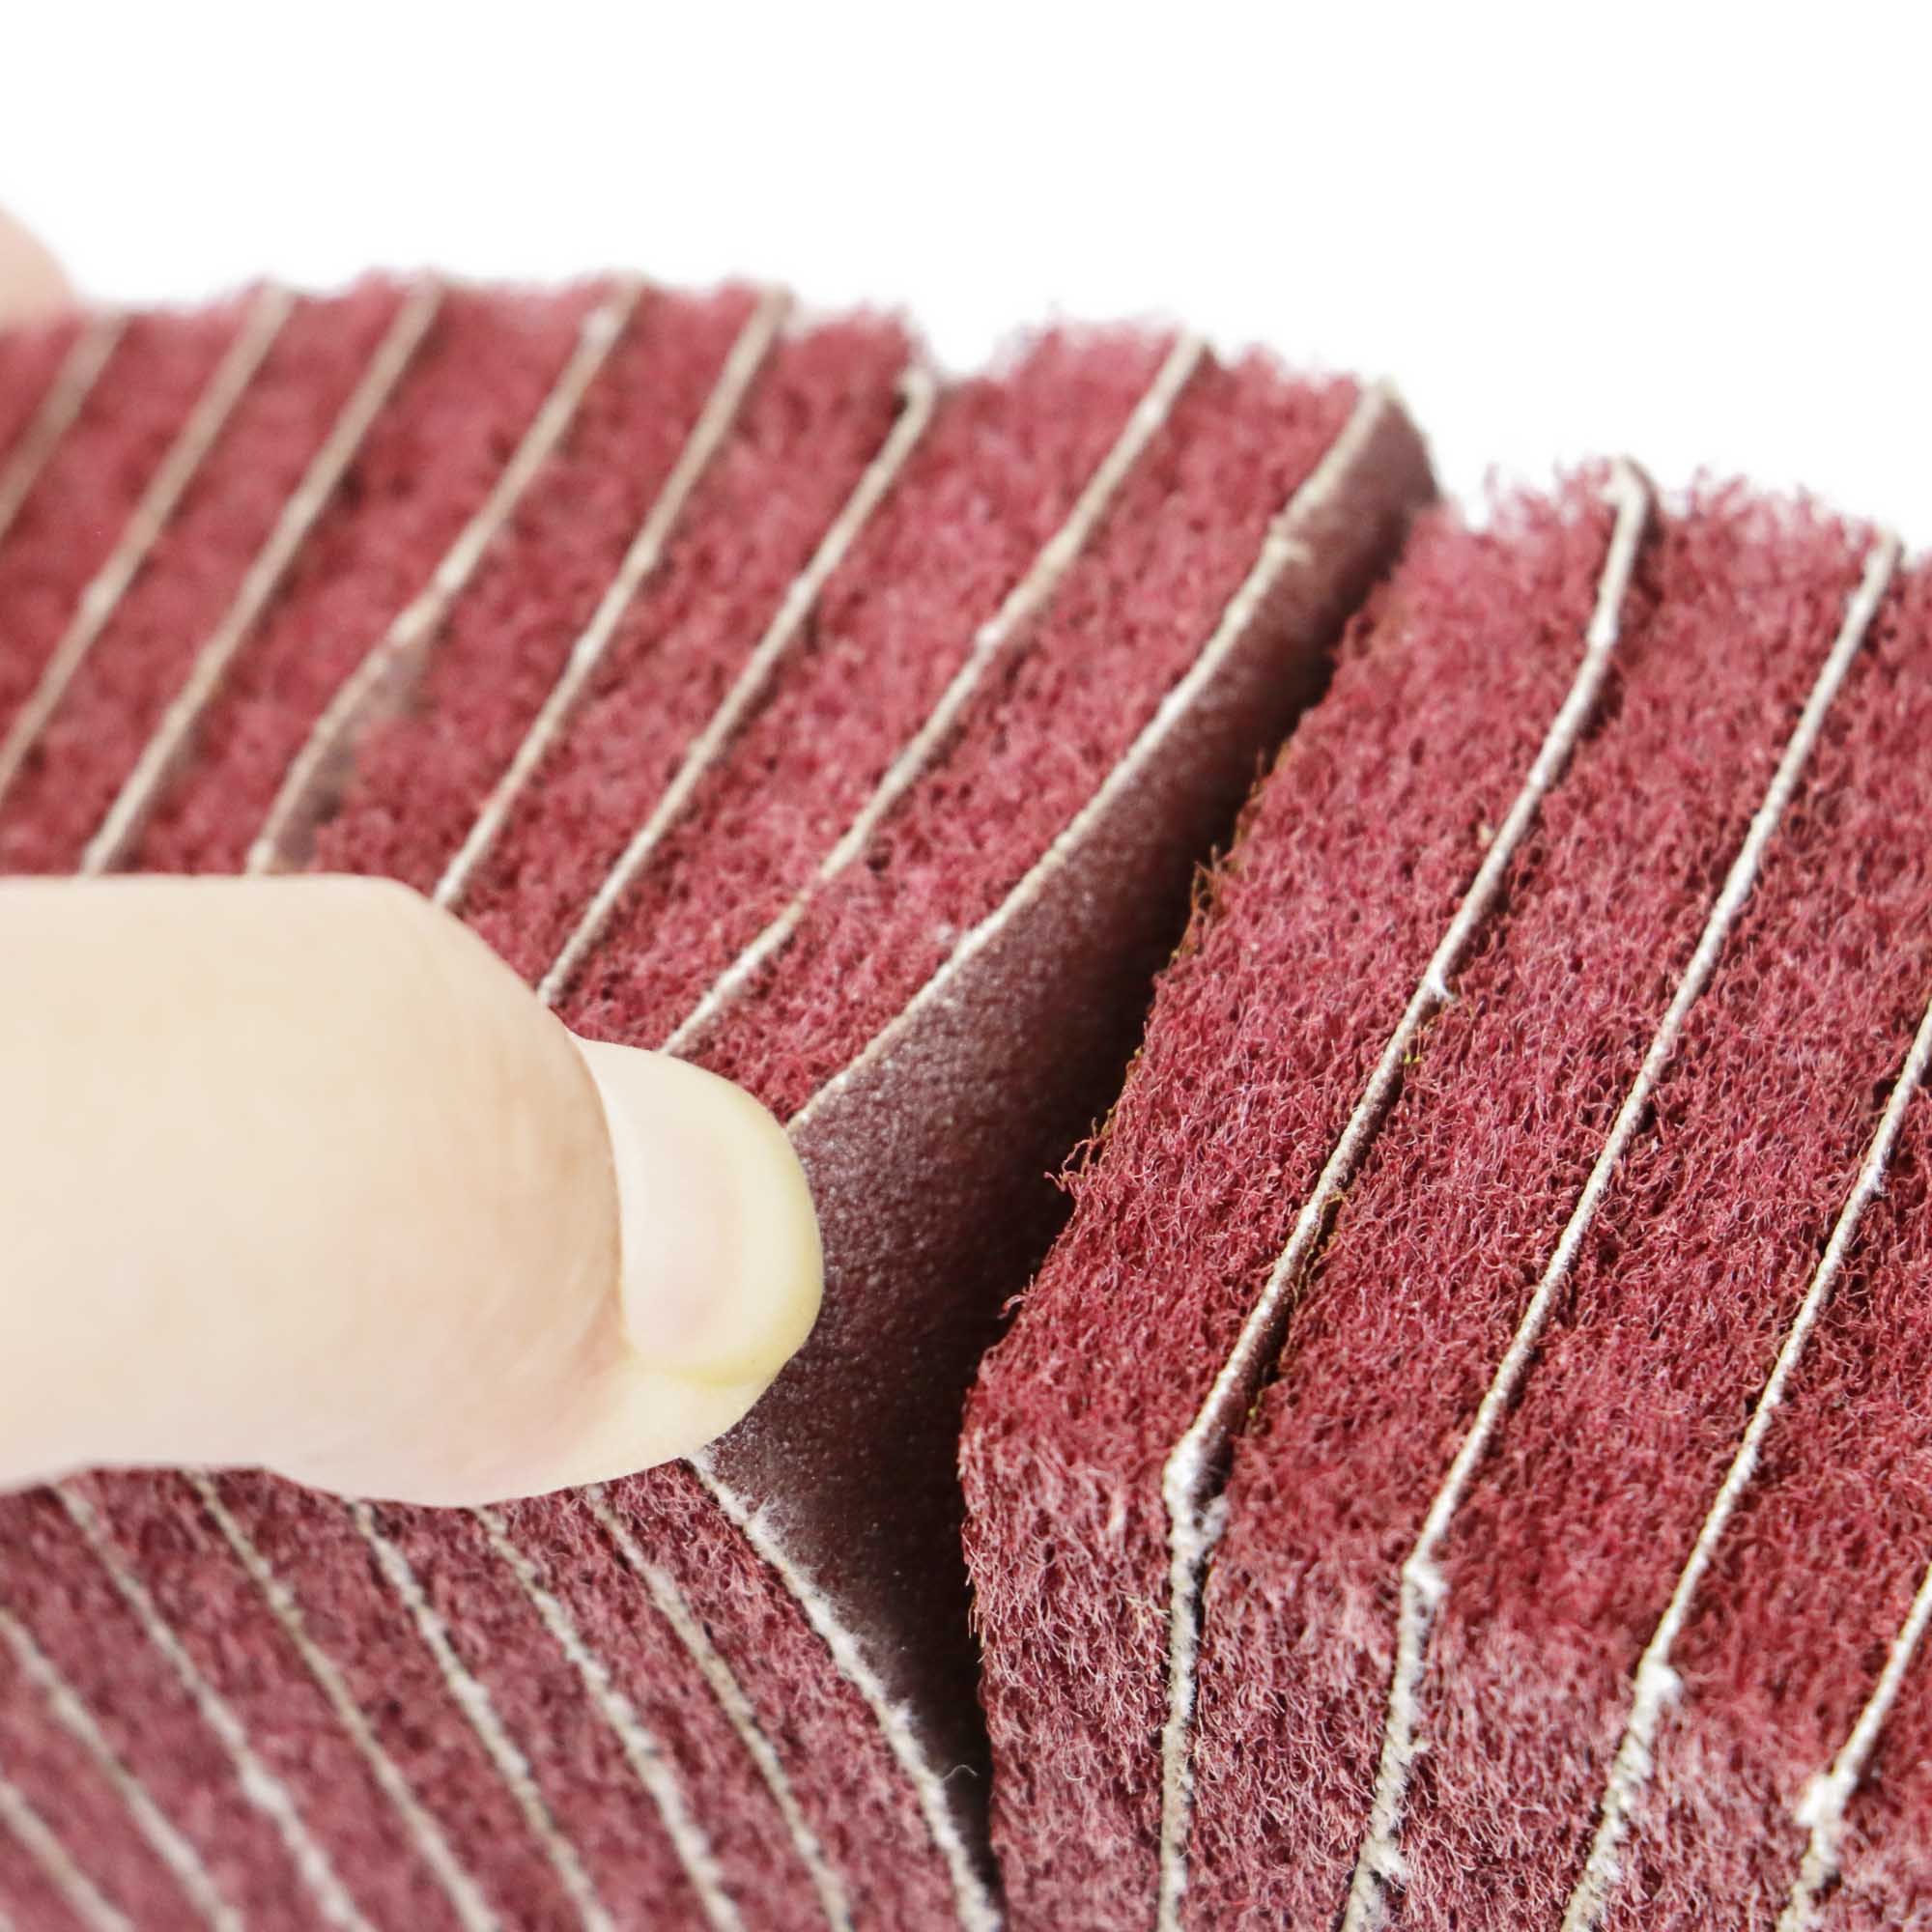
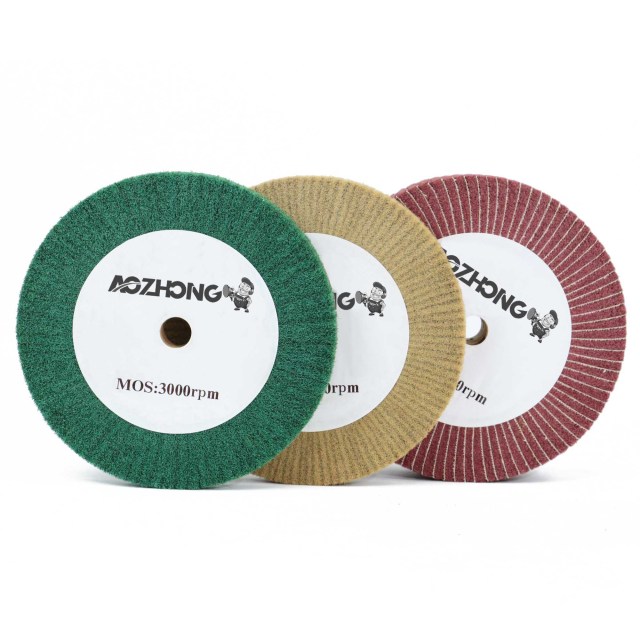
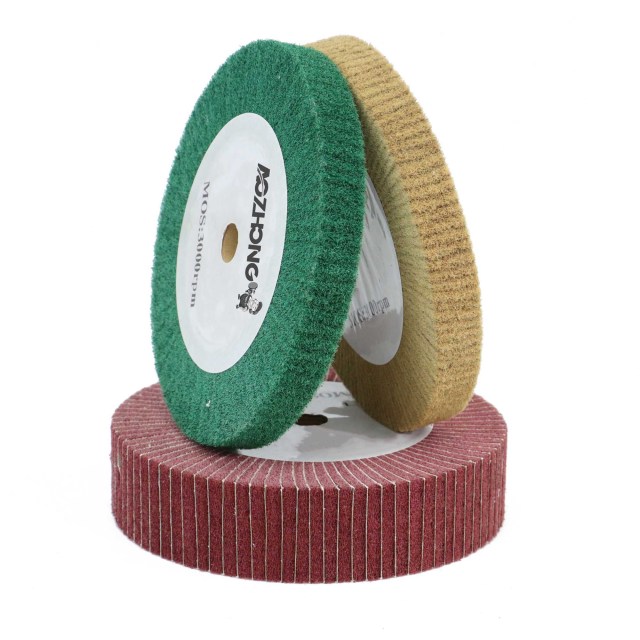
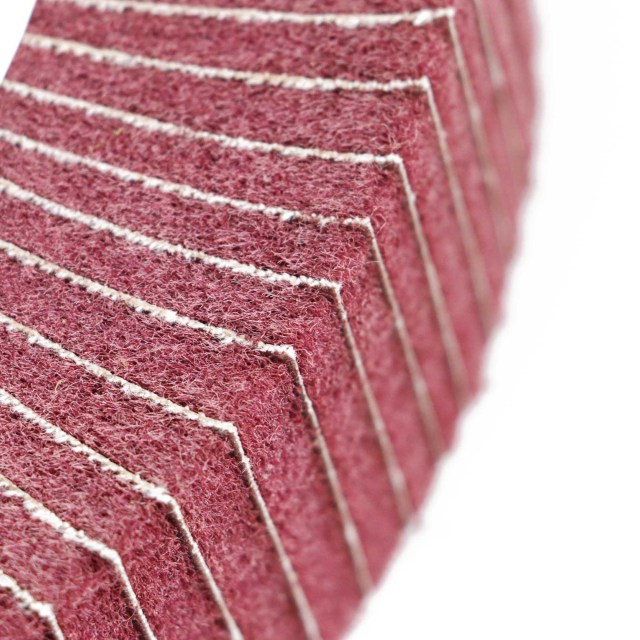
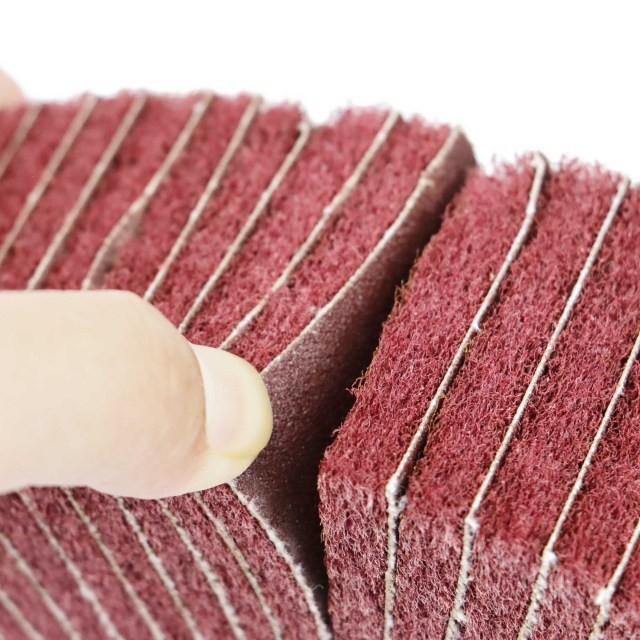
The Aozhong Interleaved Non-Woven Flap Wheel combines non-woven abrasive flaps with abrasive cloth interlayers arranged around a centre hub. The cloth flaps contribute cutting action, while the non-woven flaps participate in surface conditioning and scratch blending.
This combination flap wheel is intended for metal cleaning, surface refinement, satin finishing, rust removal and preparation before polishing. Select the configuration against the workpiece, incoming surface and target result.
Aozhong manufactures abrasive products for distributors and industrial volume buyers. Material, flap dimensions and cutting arrangements can be configured around application requirements, subject to production confirmation.
Combines abrasive cloth cutting action with non-woven surface conditioning.
Provides successive contact between the flaps and workpiece during rotation.
Allows the abrasive combination to be selected around removal and finishing requirements.
Construction schematic · Flap quantity, geometry, color and mounting details follow the approved specification.
Allow contact behavior to be evaluated against workpiece shape and access.
Non-woven grade and cloth grit can be recorded independently for purchasing control.
Supports product variants for distributor ranges and industrial finishing processes.
Application suitability depends on the abrasive combination, grade, flap arrangement, speed, pressure and workpiece material. Satin finishing does not establish a mirror finish, and rust removal does not repair corrosion pits.
Specify both abrasive components when selecting an interleaf abrasive wheel:
Aozhong’s manufacturing offer supports material and flap-construction configuration for metalworking applications. Distributors can define variants around customer processes, while volume users can specify a wheel against an existing machine and finish requirement.
| Configuration Area | Buyer Information |
|---|---|
| Material | Workpiece, current abrasive and target result |
| Flap dimensions | Required wheel geometry, contact area and workpiece profile |
| Cutting arrangement | Slotting or segmentation requirements and intended function |
| Abrasive combination | Removal requirement, incoming scratches and finish reference |
| Mounting | Bore, spindle, clamping and machine information |
It includes abrasive cloth interlayers between non-woven flaps. This changes cutting action, conformity and finish. Select the combination through workpiece testing rather than assuming it will replace a non-woven-only wheel directly.
Specify the non-woven mineral, grade and density separately from the abrasive cloth mineral, grit and backing. Include the interlayer ratio and an approved sample where available.
No. The reference photograph shows MOS 3000 rpm on a sample. Confirm the rating for the exact ordered wheel. Never exceed its marked maximum operating speed, and check the mounting and equipment requirements.
Provide the outside diameter, face width, bore, workpiece material, machine details, incoming surface and target finish. Include material, flap-dimension or cutting-arrangement requirements for production review.
Record the construction and evaluate finish, processing time, wear and running behavior. Agree on dimensional tolerances, inspection requirements and configuration-change handling before placing a volume order.