Aluminum is widely used in automotive parts, metal fabrication, transportation equipment, machinery, furniture, and other industrial products.
However, sanding aluminum is different from sanding many harder metals.
One common problem is abrasive loading. Aluminum swarf can collect between abrasive grains and cover the cutting surface. When this happens, a sanding disc may stop cutting effectively even though the abrasive grains are not completely worn.
The correct abrasive therefore needs to do more than remove material.
For aluminum finishing, buyers should consider:
Material removal → Loading control → Scratch refinement → Final surface requirement
At Aozhong, different abrasive structures can be used at different stages instead of trying to use one sanding product from heavy grinding through final finishing.
One of the main differences is how aluminum debris behaves during grinding and sanding.
When material builds up between abrasive grains, the disc gradually loses effective cutting area. Pressure and contact conditions can also affect how much heat is generated during grinding. OSHA notes that grinding heat depends on factors including tool speed, composition, contact area, duration, and applied pressure.
Common problems during aluminum sanding include:
This means simply choosing a more aggressive abrasive is not always the solution.
A better process should allow enough space for sanding debris to leave the cutting surface while using a grit suitable for the current finishing stage.
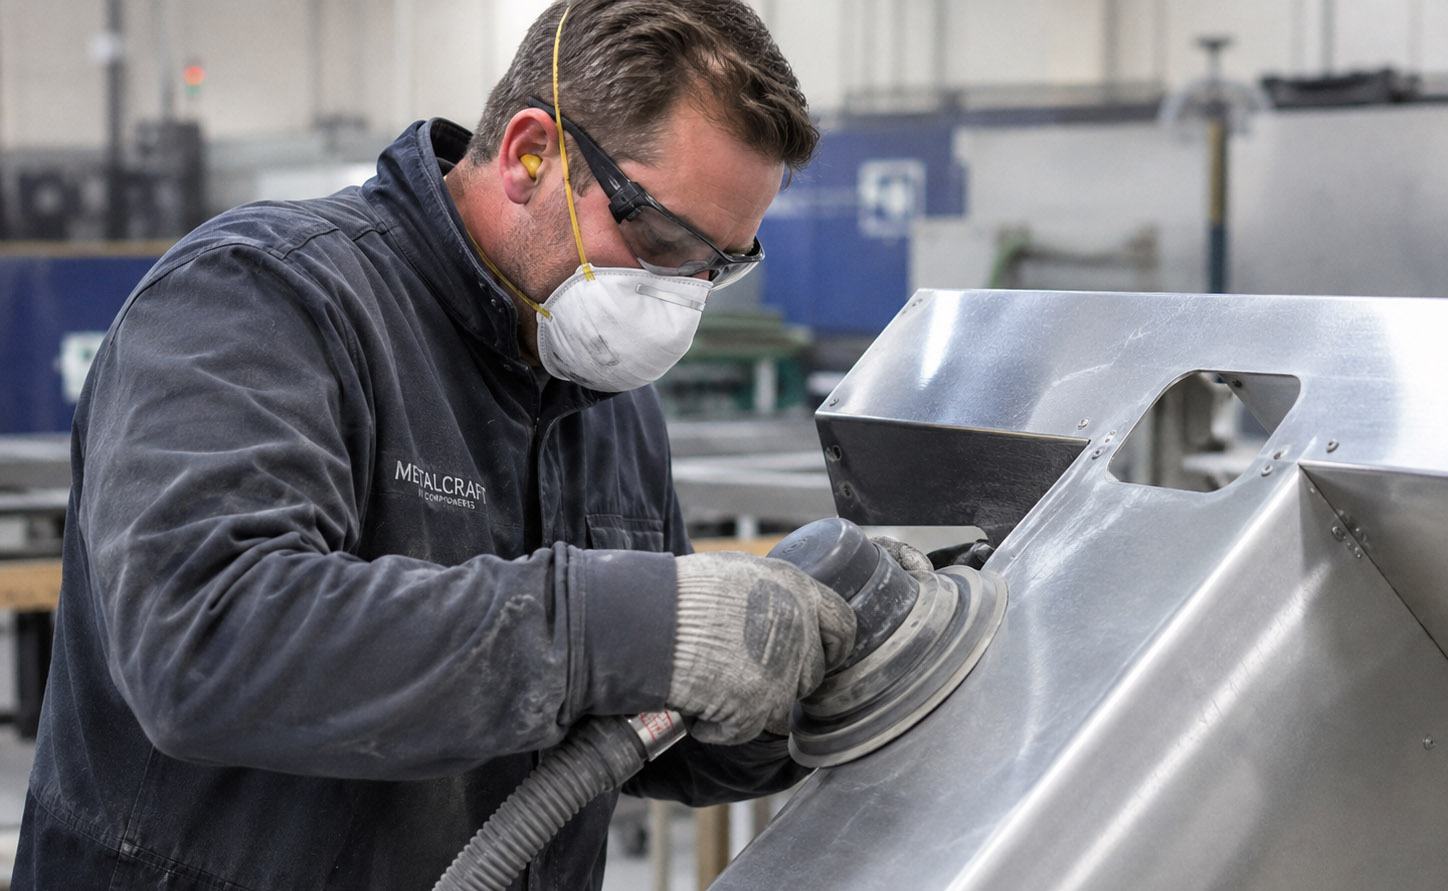
A common mistake is expecting one abrasive product to complete every stage.
Heavy material removal and final surface finishing have different requirements.
| Process | Main Purpose | Product Direction |
|---|---|---|
| Grinding | Welds, defects and heavier material removal | Grinding & Cutting Products |
| Coarse Sanding | Remove grinding marks and level surface | Coarse Sanding Disc / Abrasive Belt |
| Intermediate Sanding | Refine previous scratches | Sanding Disc |
| Fine Sanding | Prepare for finishing | Fine Sanding Disc |
| Surface Conditioning | Blend and improve surface uniformity | Non-Woven Abrasive |
| Final Polishing | Improve final appearance | Polishing Product |
For example, after reducing a weld, continuing with an aggressive grinding product may create deeper scratches than necessary.
Instead, the process can move from:
Grinding → Sanding → Scratch Refinement → Surface Conditioning
This reduces the amount of work required in later stages.
Aozhong's current product categories cover Grinding & Cutting, Sanding Discs, Abrasive Belts, Non-Woven Abrasives and Polishing Products, allowing these stages to be treated as separate operations.
There is no single best grit for aluminum.
The starting grit depends on:
A general starting framework is:
| Aluminum Finishing Stage | Reference Grit Range | Main Purpose |
|---|---|---|
| Heavy Defect / Weld Refinement | P40–P60 | Material removal |
| Coarse Scratch Refinement | P60–P80 | Reduce heavy grinding marks |
| General Surface Sanding | P80–P120 | Level and refine |
| Intermediate Refinement | P120–P180 | Reduce previous scratches |
| Fine Surface Preparation | P180–P320 | Prepare for finer finishing |
| Fine Refinement | P320–P400+ | Application-dependent finishing |
| Surface Conditioning | Non-woven grade | Blending / visual finish |
These ranges are starting references rather than fixed rules.
The main principle is:
Do not use a very fine abrasive to perform a coarse material-removal job.
If P240 is used to remove damage that should first be corrected with P80 or P120, sanding takes longer and loading may become more noticeable.
At the same time, starting too coarse creates deep scratches that require additional steps later.
Grit number is only one part of abrasive selection.
Two P120 sanding products can behave differently because of differences in backing, abrasive grain, coating structure, and dust-removal design.
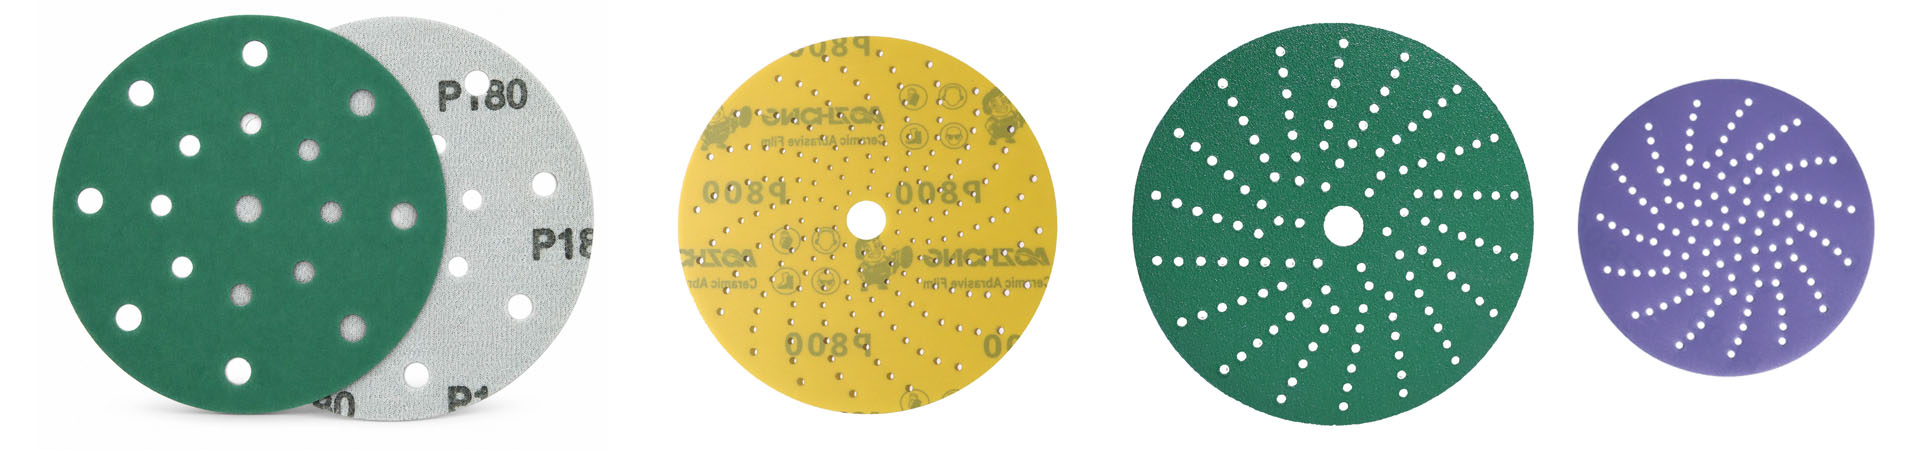
Aozhong currently supplies several abrasive structures that can be evaluated according to the aluminum finishing process.
| Abrasive Structure | Main Strength | Typical Direction |
|---|---|---|
| Paper Sanding Disc | General-purpose sanding | Surface leveling and general preparation |
| Film Sanding Disc | Stable backing | Controlled scratch refinement |
| Mesh Sanding Disc | Open structure | Dust-focused sanding and loading control |
| Abrasive Belt | Continuous sanding | Fabrication and production sanding |
| Non-Woven Abrasive | Flexible surface conditioning | Blending, deburring and finishing |
| Grinding Product | Higher removal | Weld and defect removal |
Paper sanding discs are useful for general industrial sanding.
Film-backed discs become more useful when backing stability and controlled scratch refinement are important.
They should be selected according to the required finish rather than assuming one backing is always better.
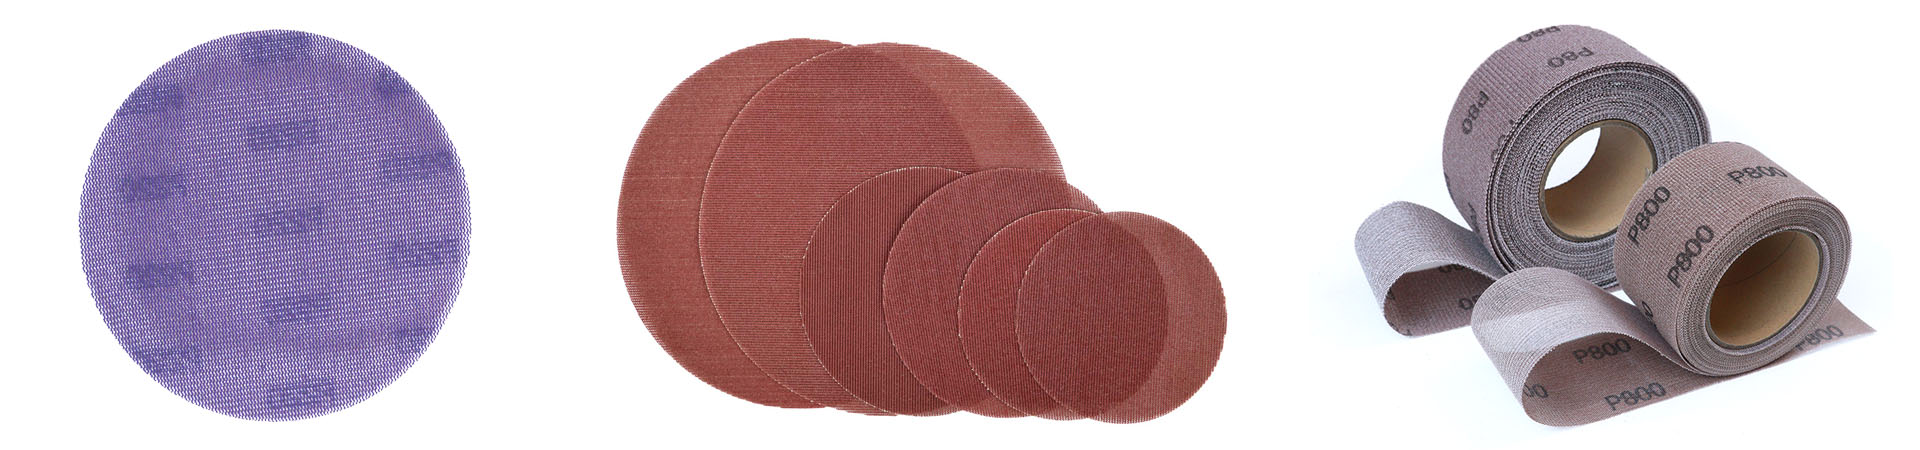
Aozhong Mesh Sanding Discs use an open fiber or polyester mesh structure designed to support airflow and sanding-debris removal. Current configurations include aluminum oxide, zirconia and ceramic abrasive options.
For aluminum applications where loading is a recurring issue, an open abrasive structure is one product direction worth evaluating.
Non-woven abrasives perform a different job.
Aozhong's non-woven products use a flexible nylon-fiber structure and are designed around cleaning, blending, oxide removal, light deburring and surface finishing rather than aggressive leveling. Available product structures include aluminum oxide and silicon carbide configurations.
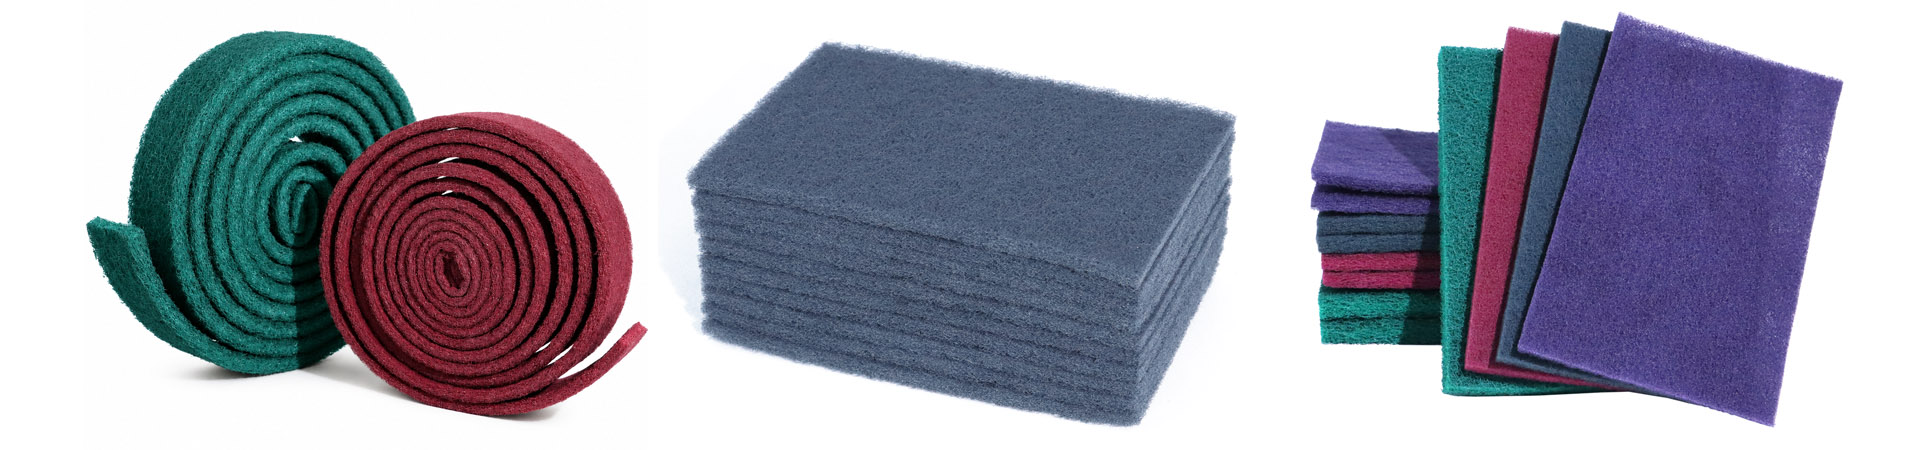
They are therefore more suitable later in the finishing process.
When a sanding disc becomes packed with aluminum debris, replacing it with another identical disc may only repeat the same problem.
Instead, check the complete process.
A grit that is too fine provides less room for larger sanding debris and may work inefficiently during heavy removal.
Use enough cutting capacity for the stage before moving finer.
More pressure does not always create better cutting.
Excessive pressure increases contact load and can contribute to heat and poor abrasive performance.
Let the abrasive perform the cut instead of forcing the machine into the workpiece.
Holding a grinder or sander in one place can increase local heat and create uneven material removal.
Maintain controlled movement and overlap.
If aluminum has covered much of the abrasive surface, additional pressure is not the solution.
Inspect the abrasive and determine why loading occurred.
For appropriate sanding stages, Mesh Sanding Discs or other structures designed to improve debris removal may help keep the cutting surface more open.
The important point is:
Loading should be treated as a process problem, not only as a sanding-disc quality problem.
Aluminum weld finishing should normally be approached as a sequence.
The objective is not simply to remove the weld as quickly as possible.
A practical process may look like:
Use the appropriate grinding or coarse abrasive product to bring the weld closer to the surrounding surface.
Avoid removing unnecessary base material.
Move to a sanding disc or abrasive belt with a suitable intermediate grit.
The goal is now scratch refinement rather than heavy weld removal.
Move through the required grit sequence until the previous scratch pattern is removed.
If a uniform industrial or decorative finish is required, move into Non-Woven Abrasives or another suitable surface-conditioning process.
| Stage | Main Goal | Abrasive Direction |
|---|---|---|
| Weld Reduction | Remove excess material | Grinding product |
| Initial Refinement | Remove grinding scratches | Coarse sanding disc |
| Intermediate Refinement | Reduce scratch depth | Medium sanding disc |
| Fine Preparation | Prepare surface finish | Fine sanding disc |
| Blending | Improve surface uniformity | Non-woven abrasive |
| Final Finish | Application-specific appearance | Conditioning / polishing |
One important rule is:
Do not expect a non-woven abrasive to remove deep grinding scratches efficiently.
Those scratches should be corrected during the coated-abrasive stages first.
Aluminum grinding and polishing also creates an issue that should not be treated simply as a sanding-performance problem.
Fine aluminum dust can present a combustible-dust hazard under certain conditions. OSHA specifically identifies aluminum among metal dusts that can become explosible when sufficiently fine material is suspended in air under the right conditions.
OSHA has also warned about grinding aluminum and ferrous materials with the same equipment because mixtures involving aluminum particles and metal oxides can create additional reaction hazards.
For industrial aluminum finishing:
This distinction is important.
A Mesh Sanding Disc may help move debris away from the abrasive surface, but abrasive dust extraction performance and safe combustible-metal dust collection are not the same question.
The facility's dust-control system needs to be designed for its actual aluminum-processing conditions.
Yes. Aluminum oxide sanding discs can be used for general aluminum sanding, scratch refinement, and surface preparation. The key is to match the grit, backing, and abrasive structure to the amount of material removal required.
Aluminum is relatively soft, and sanding debris can collect between abrasive grains. This reduces the exposed cutting area. Using the correct grit, controlling pressure, and improving debris extraction can help reduce loading.
Yes. Mesh sanding discs can be useful when abrasive loading and dust removal are major concerns. Their open structure helps sanding debris move away from the cutting surface when used with a compatible extraction system.
The correct final grit depends on the required finish and polishing process. In many cases, the surface is refined through several sanding stages before moving to a fine abrasive or polishing product. Deep scratches should be removed before polishing begins.
Yes. Non-woven abrasives are suitable for light deburring, blending, surface conditioning, and cleaning. They are better for controlled finishing than for heavy burr or weld removal.