Stainless steel surface finishing is not a single grinding step.
A fabricated stainless steel part may need weld removal, scratch refinement, surface blending, brushing, cleaning, or polishing before it reaches the required finish.
This means the abrasive should change as the surface changes.
Using an aggressive grinding product for every stage may remove material quickly, but it can also leave scratches that require more work later. Using a fine abrasive too early creates the opposite problem: sanding becomes slow and abrasive consumption increases.
For industrial users and abrasive buyers, the better approach is:
Heavy removal → Scratch refinement → Surface blending → Final finish
At Aozhong, our grinding, sanding, non-woven, and polishing products can be combined around these different stages rather than treating one abrasive as a universal solution.
Before choosing an abrasive, first decide what the finished surface should look like.
Different applications require different results.
| Surface Requirement | Main Goal | Product Direction |
|---|---|---|
| Weld Removal | Remove weld material | Grinding product |
| Heavy Scratch Removal | Level damaged surface | Sanding disc |
| Scratch Refinement | Reduce previous sanding marks | Finer sanding disc |
| Surface Blending | Make surrounding finish more uniform | Non-woven abrasive |
| Brushed Finish | Create directional surface texture | Non-woven / surface conditioning product |
| Cleaning / Oxide Removal | Remove light oxidation and contamination | Non-woven abrasive |
| Fine Polishing | Improve surface appearance | Polishing product |
This is the first rule of stainless steel finishing:
Choose the abrasive according to the required final surface, not only according to how quickly it cuts.
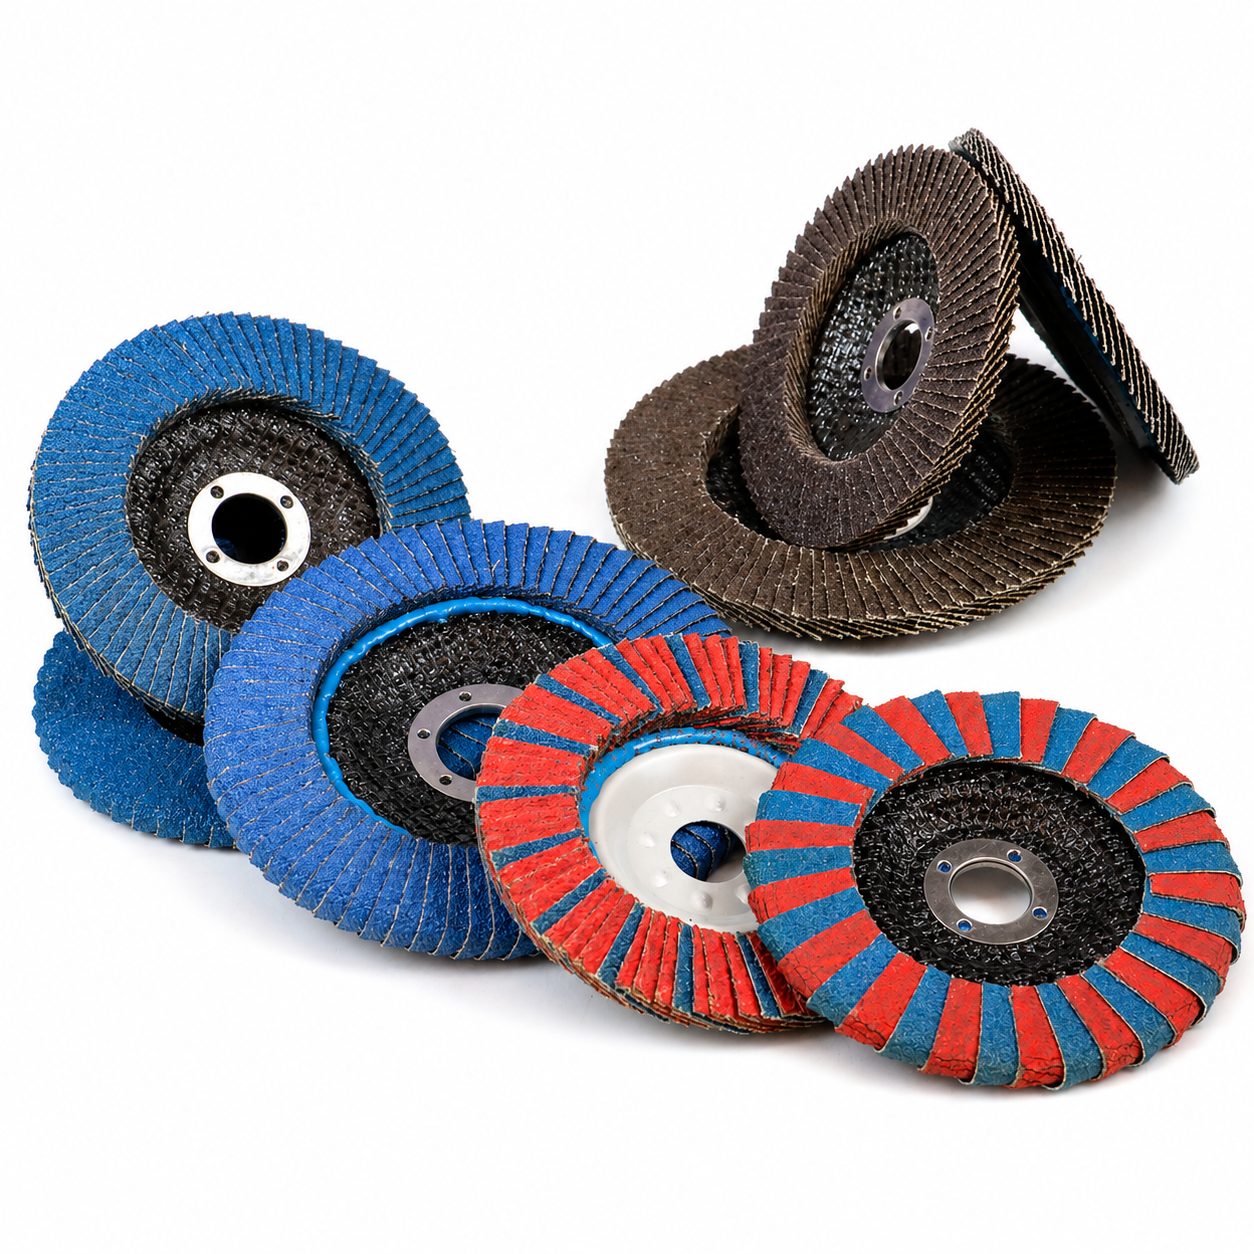
Weld removal usually requires the highest material-removal rate in the process.
At this stage, the main objective is to reduce the weld bead and bring it closer to the surrounding stainless steel surface.
Aozhong Grinding & Cutting Products can be used for the earlier material-removal stages where cutting ability is more important than final appearance.
However, aggressive grinding should stop before too much base material is removed.
Common problems include:
For this reason, heavy grinding and finishing should be treated as separate stages.
Once the weld is close to the required level, move to a more controlled abrasive.
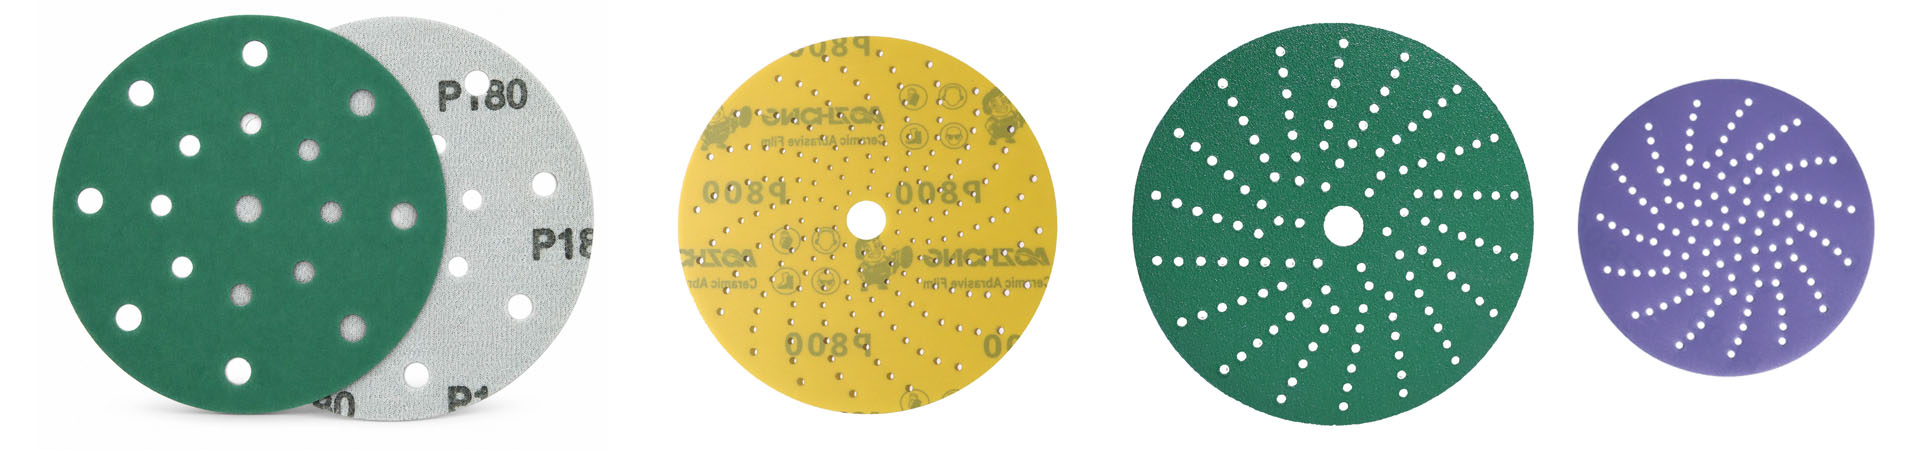
After weld grinding, the surface usually still contains visible grinding marks.
This is where sanding discs become more useful.
Compared with heavy grinding products, sanding discs provide more control when reducing scratch depth and preparing the stainless steel for blending.
A practical progression may look like this:
| Processing Stage | Typical Starting Range* | Main Purpose |
|---|---|---|
| Heavy Weld / Defect Removal | P36–P60 | Fast material removal |
| Initial Scratch Refinement | P60–P80 | Remove heavy grinding marks |
| Intermediate Refinement | P80–P120 | Reduce scratch depth |
| Fine Surface Preparation | P120–P240 | Prepare for blending or directional finish |
| Final Conditioning | Non-woven grade | Blend and control appearance |
*These ranges are general references. The starting grit depends on weld size, existing surface condition, steel thickness, tool, and required finish.
The main principle is more important than the exact number:
Each abrasive stage should remove the scratch pattern left by the previous stage.
Skipping too far between grits may leave deeper scratches underneath a finer surface.
Aozhong sanding discs can therefore be used as the transition between aggressive material removal and final surface conditioning.
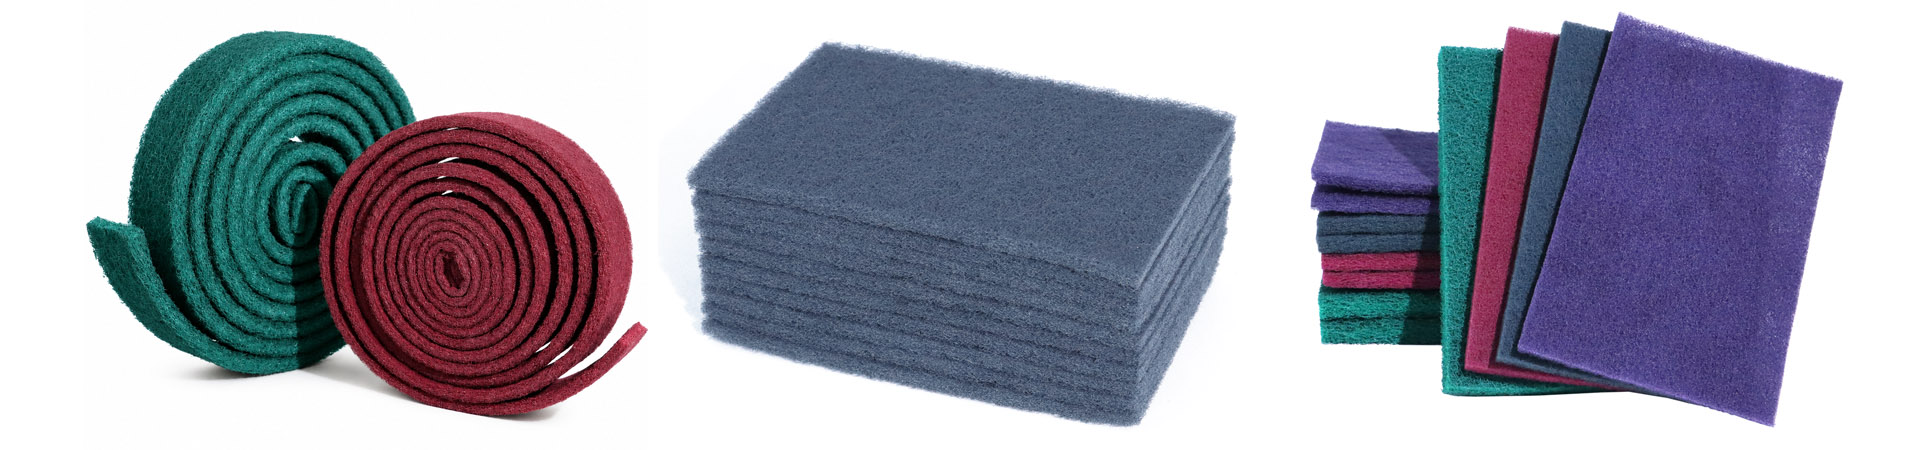
This is where coated sandpaper and non-woven abrasives perform different jobs.
Sanding discs are mainly designed around cutting and scratch refinement.
Non-woven abrasives are more useful when the objective changes toward:
Aozhong's non-woven abrasive product system includes formats such as pads, rolls, discs, and other surface-conditioning products, making them useful for different stainless steel shapes and production methods.
| Product Type | Material Removal | Surface Control | Typical Stainless Steel Use |
|---|---|---|---|
| Sanding Disc | Medium–High | Medium | Scratch removal and refinement |
| Non-Woven Disc | Low–Medium | High | Blending and conditioning |
| Non-Woven Pad | Low | High | Hand finishing and cleaning |
| Non-Woven Roll | Low | High | Custom hand pads / production use |
| Surface Conditioning Product | Low–Medium | High | Brushing and finish matching |
An important point is that non-woven abrasive grades should not be treated as direct equivalents to P-grit sandpaper.
For example, a “Fine” non-woven abrasive and P240 coated abrasive describe different abrasive structures and should not be compared only by grade name.
For brushed stainless steel, abrasive selection is only part of the process.
Sanding direction also matters.
If the final surface needs a directional grain, the abrasive should move consistently in the required direction during the later finishing stages.
Random movement may create:
A practical process is:
Remove defects → Refine scratches → Establish direction → Blend the directional finish
When using non-woven products for the final brushing stage, try to maintain:
If part of the abrasive is heavily worn while another area uses a fresh product, the surface appearance may change.
For decorative stainless steel, consistency is often more important than aggressive cutting.
Stainless steel finishing should not be treated as a test of how hard the operator can push the tool.
Excessive pressure can increase heat and may reduce control over the surface.
Common signs of poor sanding conditions include:
If cutting performance drops, check the abrasive before increasing pressure.
Ask:
The abrasive should do the cutting.
Operators should also follow the rated speed and operating instructions for the abrasive and power tool being used.
One issue that should not be ignored is contamination from carbon steel or other materials.
Abrasive products, brushes, tools, or work surfaces previously used on ordinary steel may carry ferrous particles onto stainless steel.
These particles can later contribute to visible contamination or corrosion problems on the finished surface.
For stainless steel processing, good practice includes:
For B2B buyers, this also means that abrasive identification and packaging matter.
Clearly separating products intended for different materials can reduce incorrect use in the workshop.
For manufacturers and distributors, it is rarely useful to sell one abrasive as suitable for every stainless steel finishing stage.
A more practical product system is:
| Stainless Steel Process | Product Direction | Main Function |
|---|---|---|
| Weld Removal | Grinding & Cutting Product | Material removal |
| Heavy Scratch Removal | Coarse Sanding Disc | Surface leveling |
| Scratch Refinement | Medium / Fine Sanding Disc | Reduce previous scratches |
| Surface Blending | Non-Woven Abrasive Disc | Blend processed area |
| Hand Finishing | Non-Woven Pad / Roll | Corners and manual finishing |
| Brushed Finish | Surface Conditioning / Non-Woven Product | Directional finish |
| Final Appearance Improvement | Polishing Product | Fine finishing / polishing |
This is also a more practical way to understand Aozhong's stainless steel abrasive range.
Polishing products are used when the process moves toward a finer final appearance.
The products do not need to compete with each other because they solve different problems.
Stainless steel finishing should be treated as a sequence rather than a single grinding operation.
Use grinding products for weld and material removal, sanding discs for scratch refinement, non-woven abrasives for blending and brushed finishes, and polishing products when a finer final appearance is required.
The main objective is to use enough cutting power at the beginning without creating unnecessary finishing work later.
For industrial users and B2B buyers, the right abrasive system should balance material removal, scratch control, surface consistency, heat control, and the required final finish.
Practical guidance for abrasive selection, scratch refinement, surface blending and heat control when processing stainless steel.
Yes. Aluminum oxide sanding discs can be used for general stainless steel sanding and scratch refinement. For heavier removal or longer production runs, buyers may also consider other abrasive structures depending on the application.
There is no single universal grit. A common process is to remove deeper scratches first with a coarser abrasive, then move through finer grits before using a non-woven abrasive to create a more uniform directional finish.
The most common reason is that the next abrasive is too fine to fully remove the scratch pattern from the previous stage. Contamination, worn abrasives, uneven pressure or skipped grit steps can also leave visible scratches.
Non-woven pads are better suited to blending, cleaning, light oxide removal and surface conditioning. Heavy weld removal normally requires a grinding or sanding product first, followed by non-woven abrasives for refinement.
Control heat by using the correct abrasive, avoiding excessive pressure, keeping the tool moving and replacing loaded or worn abrasives. Always use the abrasive and power tool within their rated operating conditions.